Multi-Supplier Consolidation and Container Loading from Yiwu: Carton Mixing, Labeling and Damage Control for Importers
This article is written for small and mid-sized importers, cross-border ecommerce sellers running Amazon or independent Shopify stores, discount-chain and dollar-store buyers, and first-time overseas purchasers placing their initial orders from China. When you buy from more than one Yiwu supplier, the goods do not arrive on your doorstep by themselves; dozens of small cartons from separate booths must be gathered, mixed, marked and packed into one container without losing track of which box holds what. The purpose of this guide is to show how to consolidate multi-vendor shipments from Yiwu into a single sea container with controlled carton mixing, a traceable labeling system, and practical damage-control discipline from warehouse intake to sealed door.
Why Yiwu Sourcing Is Naturally Multi-Supplier
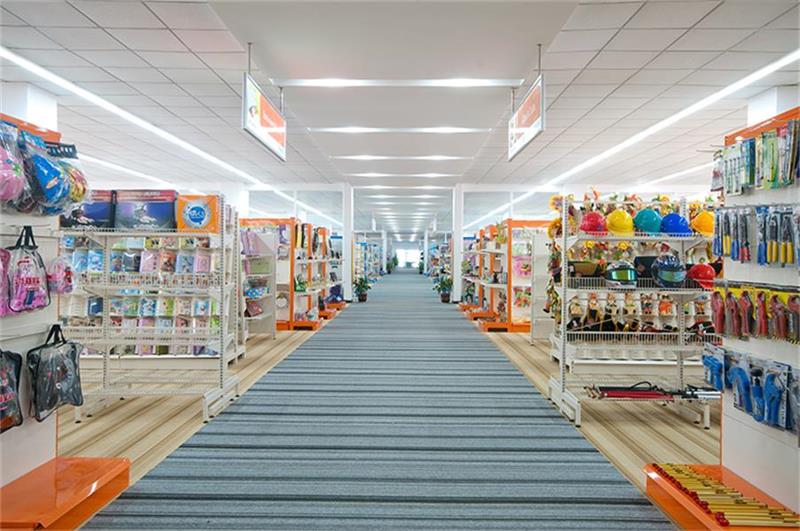
The Yiwu International Trade Market is organized as a dense grid of independent booths, and each booth typically specializes in a narrow product slice rather than acting as a full catalog factory. A buyer building a mixed assortment for a discount store or an online brand will therefore place ten, thirty or even eighty separate purchase orders across different vendors in the same trip. Single-item minimum order quantities are famously low, which is a blessing for assortment breadth but a structural reason why no single supplier can fill the whole container.
Categories are scattered physically and commercially: hardware in one district, seasonal decorations in another, household cleaning in a third, socks and apparel accessories elsewhere. Because each booth carries its own stock, lead time and packaging habit, the importer is forced into a multi-supplier reality from day one. Consolidation is the logical response, and it saves money in three concrete ways.
First, freight: shipping one full container load is almost always cheaper per cubic meter than paying for many less-than-container loads or dozens of parcel shipments. Second, customs workload: a single consolidated declaration replaces many separate filings. Third, clearance complexity: one importer of record, one entry, one set of handover documents reduces the points where a shipment can stall. The trade-off is risk. When cartons from unrelated vendors sit side by side, the responsibility interface between suppliers becomes blurred, carton counts are harder to reconcile, mixed stacking invites breakage, and inconsistent paperwork across vendors can trigger a customs hold. Managing those risks is the subject of the rest of this guide.
Pre-Conditions Before You Consolidate
Consolidation fails when it starts too early, before the inputs are fixed. Lock the following conditions before any carton moves toward the loading bay.
Freeze the SKU and supplier list. A moving target destroys the loading plan because every added or deleted item changes volume, weight distribution and carton count. Record each supplier's confirmed lead time and its historical stockout probability; a vendor with a 20 percent chance of short delivery should be flagged so the plan absorbs the gap rather than discovering it at the dock. Confirm whether packaging is unified: the outer carton material, ply count and edge-crush strength must be comparable if cartons will share a stack, or weak boxes will crush under strong ones. Decide whether palletizing is allowed by the supplier and by your destination warehouse handling; pallets simplify loading but consume payload and may be rejected by some receivers.
Name the destination port and the customs clearance entity before booking, because the entity that appears on the bill of lading must match the licensed importer at arrival. Finally, verify whether the HS codes across your mixed goods can be consolidated into a single declaration; some categories must be declared separately, and the exact grouping rules are subject to the latest official notices from the destination customs authority, so confirm the current position with your broker rather than assuming last year's practice still applies.
Carton Marking and Labeling System
A reliable carton marking system is the backbone of any mixed container, because once the door closes, the only way to know what is inside a box is the mark on its face. Build one system and force every supplier to use it; do not let vendors keep their own.
- Main mark (front face) should carry the consignee name and address, the destination port, the carton number, the SKU code, the product name, the quantity per carton, the gross and net weight, the carton volume, and the country of origin.
- Side mark should repeat the carton number, SKU, gross and net weight, and a handling icon such as "this way up" or "do not stack" where relevant, so the box is identifiable from any orientation in the stack.
- Carton number coding rule: combine a supplier code, the SKU, and a serial number, written as SUPPLIER-SKU-001, SUPPLIER-SKU-002 and so on, so each box is unique and traceable to its vendor and item.
- Do not use each supplier's own numbering scheme, because conflicting sequences make reconciliation impossible and guarantee that someone opens the wrong carton at delivery.
- Barcode and scanning reconciliation: print a scannable barcode encoding the carton number, scan every carton at warehouse intake and again at loading, and reconcile the scan list against the packing list in real time.
- For mixed loading, enforce one box one code and make the code traceable: every carton maps to exactly one supplier, one SKU and one position in the container plan, so a damage claim or a short delivery can be pinpointed without opening the whole shipment.
Container Loading Layout Principles
How cartons are placed inside the container decides whether they arrive intact. The first principle is weight distribution: heavy goods go on the floor and toward the front near the container head, light and bulky goods go on top. This lowers the center of gravity and protects weak cartons from compression.
Fragile products and cartons with low board strength belong near the top or on a dedicated pallet away from the load above them. Liquids, powders and products containing batteries must be isolated: batteries require correct UN marking and a declared dangerous-goods file where applicable, liquids need leak-proof inner packing and upright orientation, and powders need sealed liners, all with the supporting documents attached before loading. Respect stacking layer limits printed on the carton and apply "do not stack" or "this way up" icons where the vendor specifies them.
Use dunnage and lashing to stop movement: air bags, cardboard fillers and strapping keep the load from shifting during transit, and a tight load is a load that does not hammer itself to pieces. Capture photographic evidence at defined nodes: the empty container showing a clean, dry floor, the half-loaded state showing weight placement, the full loaded state before closing, and a clear shot of the seal number as the door is locked. These images are your proof if a dispute arises later.
Main Sources of Damage and Control Methods
Most container damage is predictable, and each predictable cause has a corresponding control with a measurable acceptance standard. Treat the following as a checklist, not advice.
Insufficient outer carton strength. Cause: board too thin for the stack height and transit vibration. Control: specify ply count and edge-crush value matched to your stacking plan and confirm with a test report. Acceptance: carton holds its shape under the planned load with no corner collapse at intake.
Internal voids. Cause: loose product inside an oversized carton rattles and bruises. Control: choose carton size close to product dimensions and add internal filler. Acceptance: no audible movement when the sealed carton is shaken.
Stacking over limit. Cause: loaders exceed the printed layer limit. Control: mark limits on the carton and brief the loading team. Acceptance: observed stack height never exceeds the printed maximum.
Unstable pallets. Cause: uneven stacking or shrink-wrap failure. Control: center the load, wrap securely, stretch-wrap corners. Acceptance: pallet does not tilt when pushed at the base.
Handling during loading and unloading. Cause: dropping, dragging and forklift impact. Control: train handlers, forbid throwing, use spotters at the ramp. Acceptance: zero carton punctures or crush marks recorded at intake versus at delivery.
Sea moisture. Cause: container sweat and high humidity. Control: place desiccant bags at a rate matched to container volume and transit season, and line the floor with a moisture barrier film. Acceptance: interior humidity indicator stays in the safe range and cartons arrive dry.
Tip: never accept a supplier's promise that cartons are "strong enough" without a documented burst and edge-crush test value matched to your stacking plan and transit mode.
Seal and handover responsibility. Cause: an unclear chain of custody lets damage get blamed on the wrong party. Control: record the seal number, the sealer's name and the time, and photograph the sealed door. Acceptance: seal number at departure matches the number at arrival, with a signed handover note bridging the gap.
Quantity and Responsibility Interface Management
Quantity accuracy is where multi-supplier loads most often break down, because each vendor delivers to its own count and the container total is only as good as the reconciliation between them. Count every carton at warehouse intake against the supplier packing list and flag discrepancies immediately while the vendor is still reachable.
Treat packing list reconciliation as a hard gate rather than a formality. Reconcile the consolidated packing list against the actual loading list carton by carton; the two must match before the door closes. Define short-shipment and over-shipment rules in advance: a short delivery is charged back to the responsible supplier using the intake record, while an over delivery is either rejected, accepted at a pre-agreed price or set aside, never silently mixed in. Split responsibility clearly: each supplier owns the count and condition of its own cartons up to the point of intake, and the consolidator owns the loading plan and the sealed container.
Inspection should happen at two nodes. Inbound inspection verifies carton count, outer condition and marking at the moment of receipt. Pre-loading sampling verifies a statistical sample of cartons for content and damage before they enter the container. Use a recognized sampling method: set an acceptable quality level and a sample size derived from the lot size, inspect for defined major and minor defects, and accept or reject the lot by comparing the observed defect count to the limit; the exact sampling levels and defect classifications are subject to the applicable standard edition and your contract, so state the method in writing rather than relying on a generic phrase.
Document Consistency
A container can be perfectly packed and still held at the border because the papers disagree. The commercial invoice, packing list, bill of lading and certificate of origin must carry consistent values for product name, number of packages, gross and net weight, volume and consignee. A mismatch between the packing list carton count and the bill of lading package count is a classic trigger for a customs hold.
The consequences of inconsistency are concrete: clearance delay while officials reconcile the discrepancy, physical inspection that opens and re-seals cartons, and amendment fees to correct the documents after the fact, often borne by the importer regardless of which vendor caused the error. Build a single master list and generate every document from it so the fields cannot drift apart, and review the draft set as one package before the vessel cuts off.
Pre-Loading Checklist
Confirm the following items before the container is released for loading. This list is the difference between a controlled shipment and a lucky one.
- Each supplier's confirmed lead time and a written plan for stockout or late delivery, including who absorbs the gap.
- Outer carton specification and strength test value recorded and matched to the stacking plan.
- Carton marking fields confirmed and the coding rule issued to every supplier in writing.
- Pallet plan decided, including pallet size, wrap method and whether the receiver accepts pallets.
- A loading sequence diagram showing which cartons load first, where heavy goods sit and where fragile goods sit.
- Dangerous-goods, battery and liquid documentation prepared and pre-cleared with the carrier where required.
- Seal number recorded with the sealer name and the time of sealing.
- Photographic nodes scheduled: empty, half, full and sealed door.
- Cargo insurance confirmed with covered perils and declared value before loading.
- Draft document set reviewed for field consistency across invoice, packing list, bill of lading and certificate of origin.
- Destination port clearance requirements confirmed with the broker, including importer of record details.
- An exception-handling procedure for rain-wet cartons, broken boxes and missing cartons at the dock.
- Desiccant quantity and moisture barrier film confirmed against container volume and transit season.
- Final carton count reconciled between scan record, packing list and loading plan before door closure.
Common Sourcing Mistakes
Importers repeat the same avoidable errors when consolidating from Yiwu. Recognize them before they cost you a shipment.
- Starting consolidation before the SKU and supplier list is frozen, then adding cartons that blow up the loading plan at the last minute.
- Letting each supplier keep its own carton numbering, so nobody can tell which box is which once they are mixed.
- Ignoring outer carton strength and assuming all boxes survive the same stack height and ocean vibration.
- Skipping photographic and seal evidence, then having no proof when damage or shortage is disputed.
- Treating document consistency as a formality, only to face a customs hold from a one-carton mismatch.
- Placing fragile or liquid goods without isolation or the required dangerous-goods or battery paperwork.
- Failing to define short-shipment responsibility, so a missing carton becomes an unpaid argument after the vessel sails.
Supplier and Agent Vetting Questions
Before you hand a consolidation and loading job to a supplier or a sourcing agent, ask the following questions and judge the answers against your own risk tolerance.
- Can you provide a written consolidation plan that shows carton count, weight and volume per supplier before booking?
- What is your standard carton marking format, and will you enforce a single coding rule across all my vendors?
- Do you perform scanned intake counting, and can you produce a reconciled scan list against the packing list?
- What stacking and loading rules do you apply for heavy, fragile, liquid and battery-containing goods?
- What photographic and video evidence nodes do you capture, and in what format are they delivered?
- How do you handle short shipment, over shipment and damaged cartons discovered at intake?
- Can you generate a consistent document set from one master list across invoice, packing list and bill of lading?
- What cargo insurance do you arrange, what perils are covered, and what is the declared value basis?
- How do you record and protect the seal number and the handover chain of custody?
- What is your procedure when rain, a broken box or a missing carton appears at the loading dock?
FAQ
How many suppliers can realistically share one Yiwu container?
There is no fixed limit; the practical constraint is total volume and weight against the container capacity and the stability of your loading plan. Importers routinely mix twenty to eighty vendors in a single forty-foot high-cube box when the carton marking system is consistent and the loading sequence diagram is respected. The number matters less than whether every carton is uniquely coded, counted at intake and placed according to weight and fragility rules.
Can different HS codes be declared together in one consolidated shipment?
Some can and some cannot, because destination customs may require certain categories to be declared separately, and the grouping rules change. The safe approach is to confirm the current position with your licensed broker and build the declaration from a single verified master list, treating the exact combinability of codes as subject to the latest official notices rather than assuming a fixed answer.
What is the fastest way to prove a damage claim after arrival?
Use the evidence captured at loading: the empty-container photo showing a dry floor, the full-load photo, the sealed-door shot with the seal number, and the signed handover note recording the seal at departure and at arrival. Combined with the one-box-one-code traceability, you can pinpoint which supplier's carton failed and whether the damage occurred before or after sealing, which decides who pays.
Should I palletize every carton in a mixed Yiwu load?
Not necessarily. Pallets speed handling and protect cartons but consume payload and may be rejected by your receiver, so decide per shipment based on carton strength, handling at both ends and cost. A common pattern is to palletize only fragile or high-value cartons and floor-load the rest, with the choice recorded in the loading sequence diagram before booking.
Related Pages
- Top 15 Cleaning Products Worth Wholesale from China
- Top 9 China Household Cleaning Products Wholesale Markets
- Best 13 China Household Cleaning Products Manufacturers
- Best 13 China Sock Manufacturers & Import Guide
Post time: Oct-22-2026